Our R&D Center was established on November 26, 2021.
Equipped with advanced facilities and skilled researchers, it develops a range of technologies for sustainable energy and resource recycling.
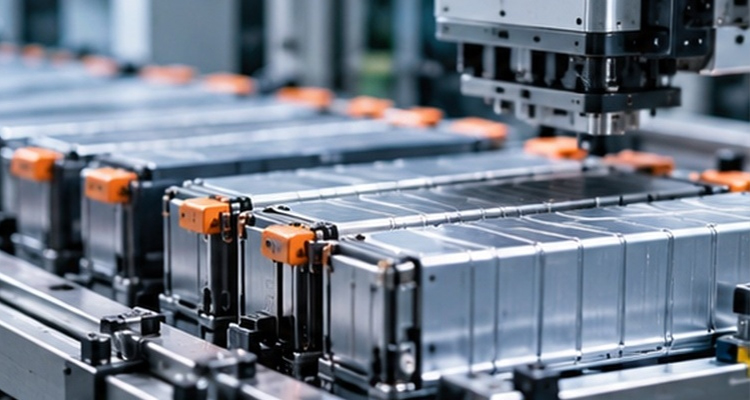
Our R&D Center is developing innovative processes to reduce carbon emissions from the pre-treatment of spent batteries.
Our goal is to minimize the environmental impact of battery recycling and build more sustainable battery recycling technologies.
We are developing technology to recover and reuse the electrolyte from spent batteries.
Through electrolyte recovery, we aim to improve the quality of battery recycling feedstock while enhancing the safety and environmental performance of the pre-treatment process.
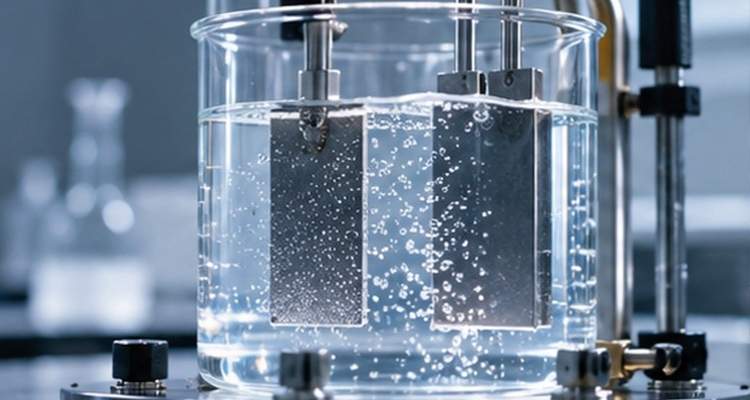
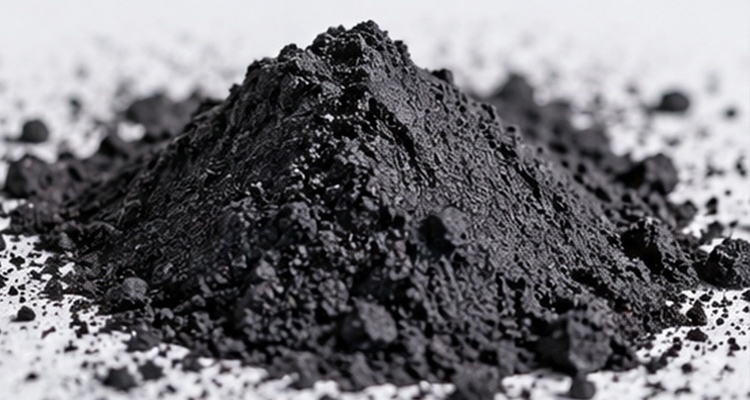
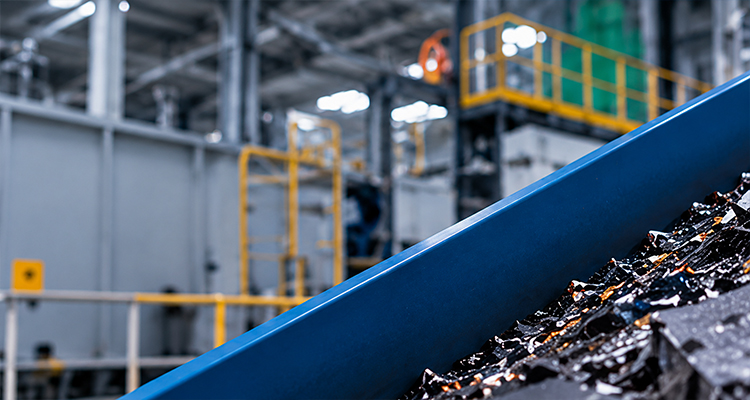
We are developing technology to produce high-grade black mass suited to downstream refining.
Black mass is the key feedstock for recovering valuable metals such as nickel, cobalt and lithium from spent batteries. By recovering the electrolyte before shredding and advancing our sorting process, we aim to reduce impurities such as aluminum and copper and improve metal recovery efficiency in downstream processes.
We are researching technologies to separate, refine and purify the main battery materials.
These technologies improve recycling efficiency and help secure high-quality recycled materials.
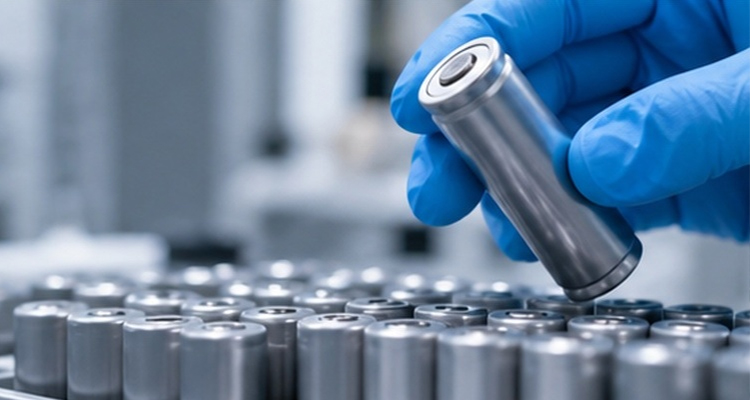
We are developing pre-treatment technology that prepares electrolyte-free cells and active materials for direct recycling.
We have supplied ton-scale samples to domestic companies.
 ENG
